
- Accueil
- Centre De Connaissances
- Composites
- Composite Tooling Solutions for Marine...
Composite Tooling Solutions for Marine Composite Manufacturing
16/09/2026
Scott Bader Technical Team
The cost of an underperforming mould builds up long before the mould is identified as the cause. It shows up as rising finishing labour, an unplanned flatting operation, and more parts held at visual approval. By the time that cost is visible in production reporting, the tool has been in service for two years and the decision behind it was taken on unit price.
Tooling comes before every composite part in a build programme, which means it sets the ceiling on the quality of those parts. Surface finish, dimensional accuracy, demould behaviour and cycle time are all decided at the mould, and none of them can be recovered cheaply further down the line. As marine structures get larger, lighter and more visually demanding, the cost of getting that decision wrong rises with them.
This article covers what a marine tooling system is made up of, how the main material options compare on accuracy, lifespan and cost, and where specification decisions feed straight into cost per part.
Why Composite Tooling Matters in Marine Manufacturing
Every composite part is formed in a mould built to the shape of that part. As set out in our composite tooling overview, moulds are usually taken from a pattern, or plug, that matches the finished component. The quality of the mould sets the quality of every part it produces.
The mould controls five things in production:
Surface finish. Any defect in the mould surface is repeated in every part taken from that tool, for as long as the tool stays in service
Structural accuracy. Bulkhead positions, stringer lines and bonding faces can only be as accurate as the tool that formed them
Dimensional consistency. A tool that moves between lifts produces parts that need shimming, trimming or rework at assembly
Production cycle times. Demould behaviour, release performance and the amount of finishing work needed after moulding are all set by the tool
Manufacturing cost. Rework, scrap and finishing labour are tooling costs, but they are recorded against other budgets
Marine manufacturing puts more pressure on tooling than most sectors. Hull and deck tools are among the largest moulds built in any industry, which makes shrinkage, distortion and postcure harder to control. Topsides and superstructures are high-gloss visible surfaces where fibre print-through cannot be accepted. Tolerances on bonded assemblies are tight, because a hull-to-deck joint has to fit within its designed bond gap. Moulds also run at high utilisation, in warm workshops, against styrenated production resins and repeated release cycles.
What a Marine Tooling System Consists Of
A production mould is a laminate built up in layers rather than a single material. Each layer does a different job, and the finished tool only performs if those layers are formulated to work together. Mixing products from different suppliers across the stack introduces adhesion and compatibility problems, and those account for a large share of tooling failures.
The plug or pattern
The mould surface can only be as good as the plug it is taken from. Money spent getting the plug finish right is recovered several times over in reduced mould finishing labour.
Plugs were traditionally built from wood, which was slow and vulnerable to changes in temperature and humidity. Current practice machines the plug directly from MDF or rigid polyurethane or polystyrene foam, then applies a fairing layer to achieve the final surface. Scott Bader supplies Crestamould T29 tooling paste at this stage, applied by spray or extrusion in thick sections and machined on multi-axis CNC to final geometry. It is strong enough to take the stresses of mould building and can be used to produce limited-run moulds directly. Crystic Primecoat and Crystic Glosscoat are then applied to give the plug a high-gloss, durable surface before release.
Tooling gelcoat
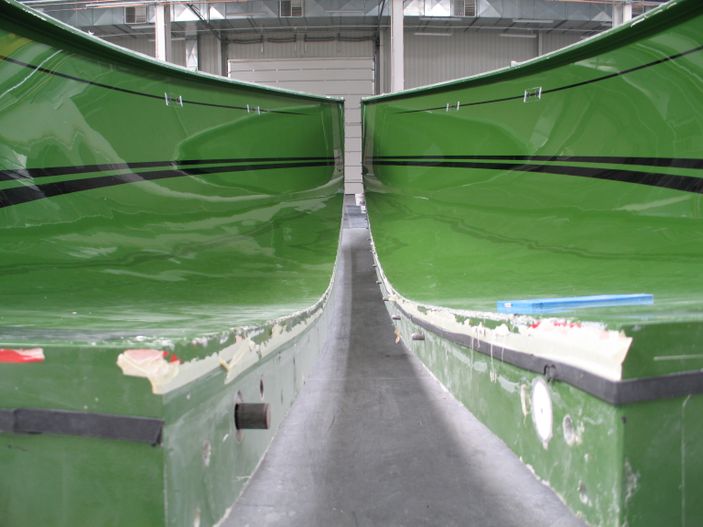
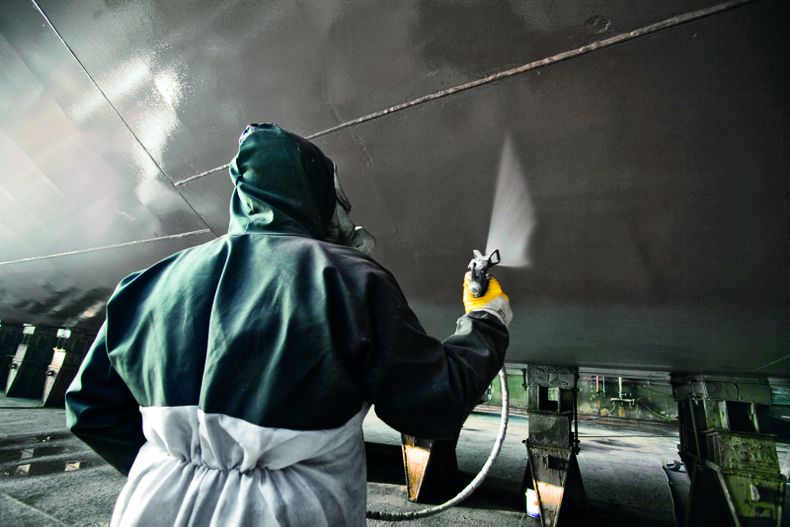
The tooling gelcoat is the working surface of the mould and the component that does most to determine how long the tool lasts. It has to hold gloss across thousands of release cycles, take the exotherm from parts moulded against it, resist styrene attack from production resins, and resist water marking.
Crestamould GC 15PA is a vinyl ester hybrid tooling gelcoat formulated for gloss retention alongside impact, heat and chemical resistance. Its viscosity profile gives even coverage with minimal drainage and low film porosity, both of which count for a lot on the vertical sections of a hull tool. Brush and spray grades are available.
Skincoat
The layer immediately behind the gelcoat controls fibre print-through, the defect that shows up as a reinforcement pattern telegraphing through a high-gloss surface. Crestamould VE 679PA is a DCPD-modified vinyl ester skincoat applied at a 2:1 resin to glass ratio, typically as a surface tissue plus 300gsm CSM, or two layers of 300gsm CSM.
Tooling laminate
The bulk laminate provides stiffness and dimensional stability. Crestamould RTR-4010PA is a pre-filled, low shrink rapid tooling resin, laminated at a minimum 3:1 resin to glass ratio in sets of four layers of 450gsm CSM, wet on wet. It contains low-profile additives that need a controlled exotherm during cure to activate and hold shrinkage in check. Layup schedule and ambient conditions are specified figures rather than guidance.
Bracing, postcure and release
Bracing or core materials are bonded to the cured laminate using a bonding paste such as Crestafix 621, with a general purpose resin as the closing skin. The completed mould should be postcured for 16 hours at 40°C or 3 hours at 80°C before demoulding from the plug. Where postcure is not practical on a large marine tool, the mould should be left to mature for 7 days at 18°C or above.
Full application parameters, including catalyst levels, film thickness and spray settings, are set out in the tooling application guide.
Tooling Materials and Technologies
Material selection is a commercial decision as much as a technical one. Three factors set the answer: how many parts the tool has to produce, how large those parts are, and whether the process applies heat.
| Material | Accuracy | Lifespan | Relative cost | Best application |
|---|---|---|---|---|
| Polyester tooling systems | Good, with higher shrinkage to manage | Moderate | Lowest | Short to medium runs, ambient cure processes, cost-sensitive programmes |
| Vinyl ester hybrid systems | High, low shrink formulations available | High | Moderate | Production marine tooling, high-gloss visible surfaces, open mould and infusion |
| Epoxy tooling systems | High, low shrinkage | High | Higher | Elevated temperature processes, high dimensional demand, prepreg work |
| Carbon fibre tooling | Very high, very low thermal expansion | High | Highest | Autoclave and oven cure, high-precision components, aerospace-derived processes |
| Machinable tooling paste | Defined by CNC accuracy | Low to moderate | Varies with volume | Plugs, patterns, prototype and limited-run moulds |
Two things are worth adding. Low thermal expansion only pays for itself where the process applies real heat, which is why carbon tooling is standard in aerospace and rare on a 24 metre hull moulded at ambient temperature. And the cheapest tool to buy is rarely the cheapest tool per part, because mould life and finishing labour outweigh the purchase price long before the tool comes out of service.
For marine work at elevated temperature, high HDT vinyl ester tooling resins such as Crystic VE671 are specified where the mould has to hold its shape against process heat.
Marine Applications
Hulls and decks
The largest tools in the programme and the least forgiving. Shrinkage, distortion during postcure and handling loads all increase with tool size, and movement in a hull tool shows up later as a deck that will not close to specification. Low shrink tooling resins and a controlled postcure regime are the main defences.
Superstructure and visible topsides
High-gloss visible surfaces, where print-through and water marking do the most commercial damage. The skincoat layer and a heat-resistant tooling gelcoat are specified mainly to control those two defects.
Interior components and small mouldings
Higher part counts across more tools, at lower margin per part. Repeatability and short lead times on replacement tooling matter more here than outright mould life.
Prototype, concept and low-volume tooling
Machined tooling paste allows a mould to be produced directly from CNC data for concept craft, one-off builds and validation work, without committing the capital for a full production tool. What you specify here is different from production tooling, as covered in the FAQ below.
The Tooling Development Process
Consultation and design review. Part geometry, draft angles, production volume, process temperature and finishing requirements are agreed before any material is specified. Design for manufacture issues cost very little to fix at this stage and a great deal once the tool is in production.
System specification. Gelcoat, skincoat, tooling resin and bonding paste are selected as a matched set, along with catalyst levels and layup schedules appropriate to the mould size and ambient conditions.
Plug preparation and mould build. Plug surface finish, gelcoat film thickness, skincoat consolidation and laminate exotherm control. Each stage has a process window, and each is a well-known failure point when that window is missed.
Postcure, release and validation. Postcure to develop full mechanical properties, then a sealing and release regime built up over the first few lifts until release performance settles down. A masking tape test after the first release confirms the release agent is still on the mould surface.
The Commercial Case for Tooling Quality
The return on tooling specification shows up in production data rather than product literature.
Reduced finishing labour. Print-through and surface defects are corrected by hand. Flatting and polishing designed out at the tool is labour taken off every part that tool produces
Lower scrap and rework. Dimensional drift in a tool shows up as parts needing adjustment at assembly, booked as rework against the part rather than against the mould
More lifts per tool. Mould life is the divisor in tooling cost per part, and extending it is usually the biggest lever available
Faster mould commissioning. Rapid tooling resins and set postcure schedules shorten the gap between finishing the plug and running the first production part
Predictable release behaviour. Pre-release and de-wetting cost time and put parts at risk
One field figure shows the range available. Gary Bates, Managing Director of Hi Spec Plastics, reported a mould built with a Scott Bader tooling gelcoat passing 4,000 lifts over a number of years with no dulling, crazing or cracking of the gelcoat surface. The difference between a tool retired at a few hundred lifts and one still running at several thousand comes down to specification and how well it was applied.
Where Technical Support Changes the Outcome
Product selection is the visible part of a tooling decision. How the mould performs over its life usually comes down to the technical work around that choice.
Trial support during the mould build. On-site support through gelcoat application, film thickness, catalyst levels and exotherm behaviour, on the actual tool and in the conditions the workshop is running in
Gelcoat application support. How consistently the gelcoat goes on is the most common difference between a tool that reaches its design life and one that does not, and it is sorted out more reliably on site than on a data sheet
Layup schedule review for large tools. Marine moulds sit at the top of the size range standard schedules were written for. Reviewing the schedule for the specific tool heads off exotherm and shrinkage problems that only appear at scale
Matched systems. Specifying gelcoat, skincoat and tooling resin formulated to work as a system takes a whole set of compatibility and adhesion risks off the table at the point of specification
Fault diagnosis. When a mould surface starts to degrade, finding the cause quickly decides whether you are looking at a repair or a rebuild. Our guidance on common gelcoat faults covers identification, causes and prevention
Scott Bader has supplied the marine industry since 1951 and brings over 70 years of composite experience to tooling specification. Our technical teams work on site with boatbuilders across the luxury, leisure and commercial sectors. Our case studies show how that support has worked in production.
Frequently Asked Questions
What is composite tooling in marine manufacturing?
Composite tooling is the mould, or tool, used to form a composite part in its finished shape. In marine production that covers hull and deck moulds, superstructure tools, interior component moulds and the plugs and patterns those moulds are taken from. The tool is a laminate in its own right, usually built from a tooling gelcoat, a skincoat and a low shrink tooling resin.
What tooling material is best for boat production?
For most production boatbuilding, vinyl ester hybrid tooling systems give the best balance of surface durability, heat resistance, dimensional stability and cost. That is why they dominate hull and deck tooling across the leisure, luxury and commercial sectors. Epoxy and carbon systems earn their higher cost in oven and autoclave work, or where a part is held to tolerances beyond what open mould marine production normally demands. In practice the specification follows the run length, the size of the part and the temperature the tool has to work at.
How long does a composite mould last?
It varies widely with specification, how well it was applied, the release regime and how hard the tool is worked. A well-specified and correctly postcured tooling gelcoat can deliver several thousand lifts without losing gloss, while a tool built on a general purpose system, applied at the wrong film thickness or released badly, can start to break down within a few hundred. Application quality is usually what decides it.
Can tooling be designed for large yacht components?
Yes, and large-format tooling is standard practice in the marine sector. What changes at scale is shrinkage control, bracing design, how the tool is postcured where oven cure is not available, and how the finished tool is handled and moved. Low shrink tooling resins and a set maturing period are the usual approach where a large mould cannot be postcured at elevated temperature.
What is the difference between prototype tooling and production tooling?
Prototype tooling is specified for a small number of parts, trading mould life for speed and lower cost, and is often machined directly from a tooling paste rather than laminated. Production tooling is specified for life, surface durability and dimensional stability across thousands of cycles, and is built as a full matched laminate system. Specifying one where the other is needed is a common and expensive mistake, and it happens in both directions.
How accurate can composite tooling be?
Accuracy is set by the plug, then either kept or lost by the tooling laminate. CNC-machined plugs and patterns hit high geometric accuracy, and a low shrink tooling system is what stops that accuracy slipping as the mould cures and matures. Shrinkage control, postcure discipline and bracing design decide whether the finished tool holds the shape it was taken from.
Conclusion
Tooling is bought once and paid for continuously. A mould that keeps its surface, holds its shape and releases predictably takes finishing labour, scrap and cycle time out of every part produced from it, for as long as it stays in service. A mould that does not becomes a running cost spread across budgets where nobody traces it back to the original specification decision.
Those decisions are taken early, in a short window, and the consequences are not obvious at the time. That is a strong argument for taking them deliberately, against matched systems and technical input rather than against price per kilogramme.
Scott Bader is a chemistry partner to boatbuilders worldwide, supplying matched tooling, composite and adhesive systems alongside technical teams who work on site rather than at a distance. Whether you are building a new hull tool, replacing an ageing mould or moving from prototype to production tooling, our marine technical team is on hand to talk through the specification.
Explore our tooling systems range →